
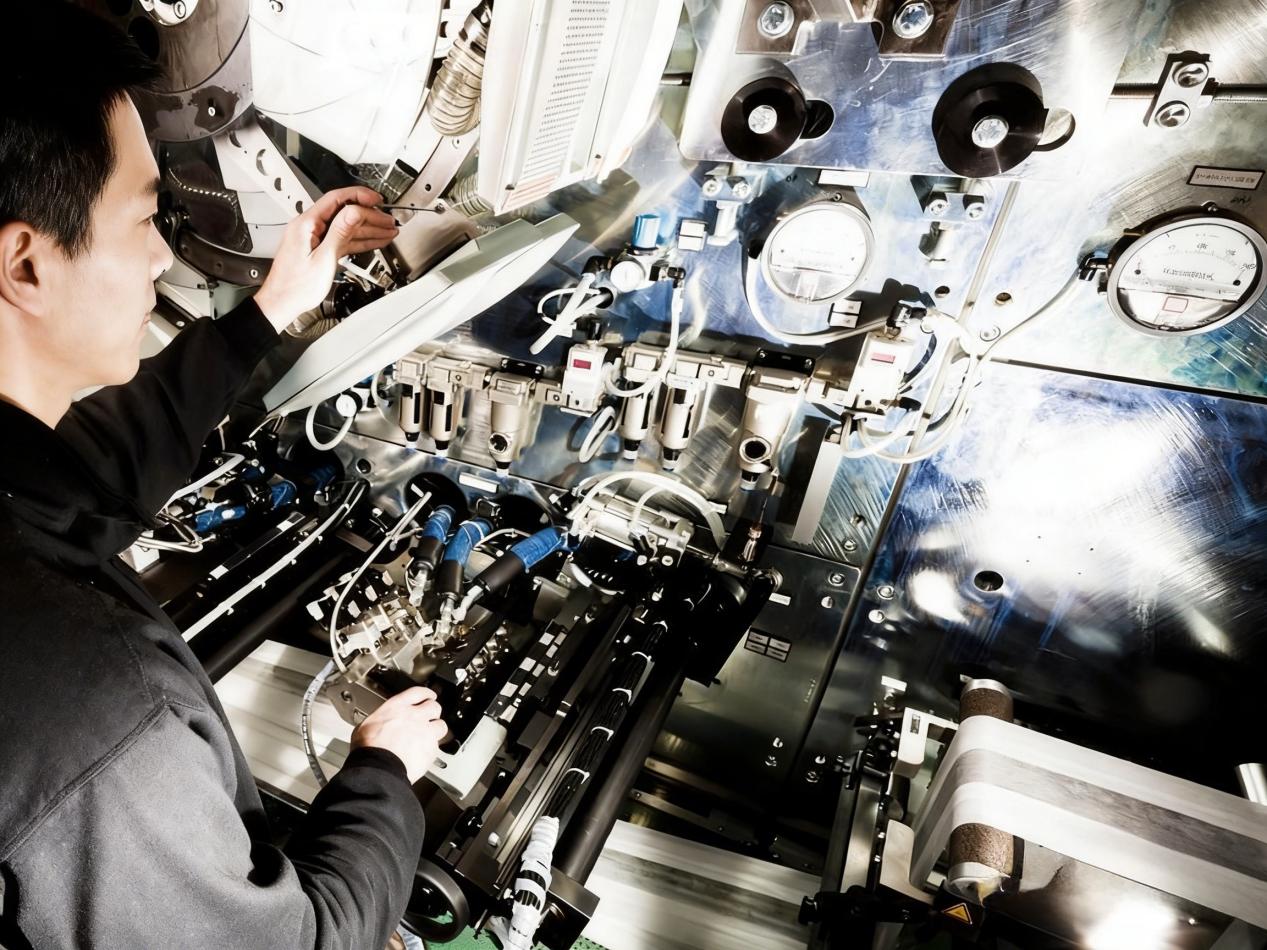
Medical disposables and personal hygiene converters face sharp capital expenditure constraints in 2026. Sourcing used nonwoven machinery offers an effective path to expand capacity at 40% to 60% lower capital expenditure than buying new production lines. However, converting raw polymer or staple fiber into surgical drapes, N95 filter media, or baby diaper topsheets leaves zero margin for technical error.
A second-hand line operating in an industrial geotextile or automotive acoustic plant cannot simply transfer to medical spunmelt or spunlace production. Trace hydraulic leaks, carbonized polymer build-up, and worn-out calender rolls can compromise an entire production run. Before committing capital or signing transfer agreements, engineering teams must execute a rigorous technical audit.
At KIMEPR, our engineering specialists conduct comprehensive technical evaluations on second-hand converting and extrusion systems worldwide. If you are assessing an operational or decommissioned line, submit an audit inquiry to our technical team to inspect the asset before issuing purchase orders.
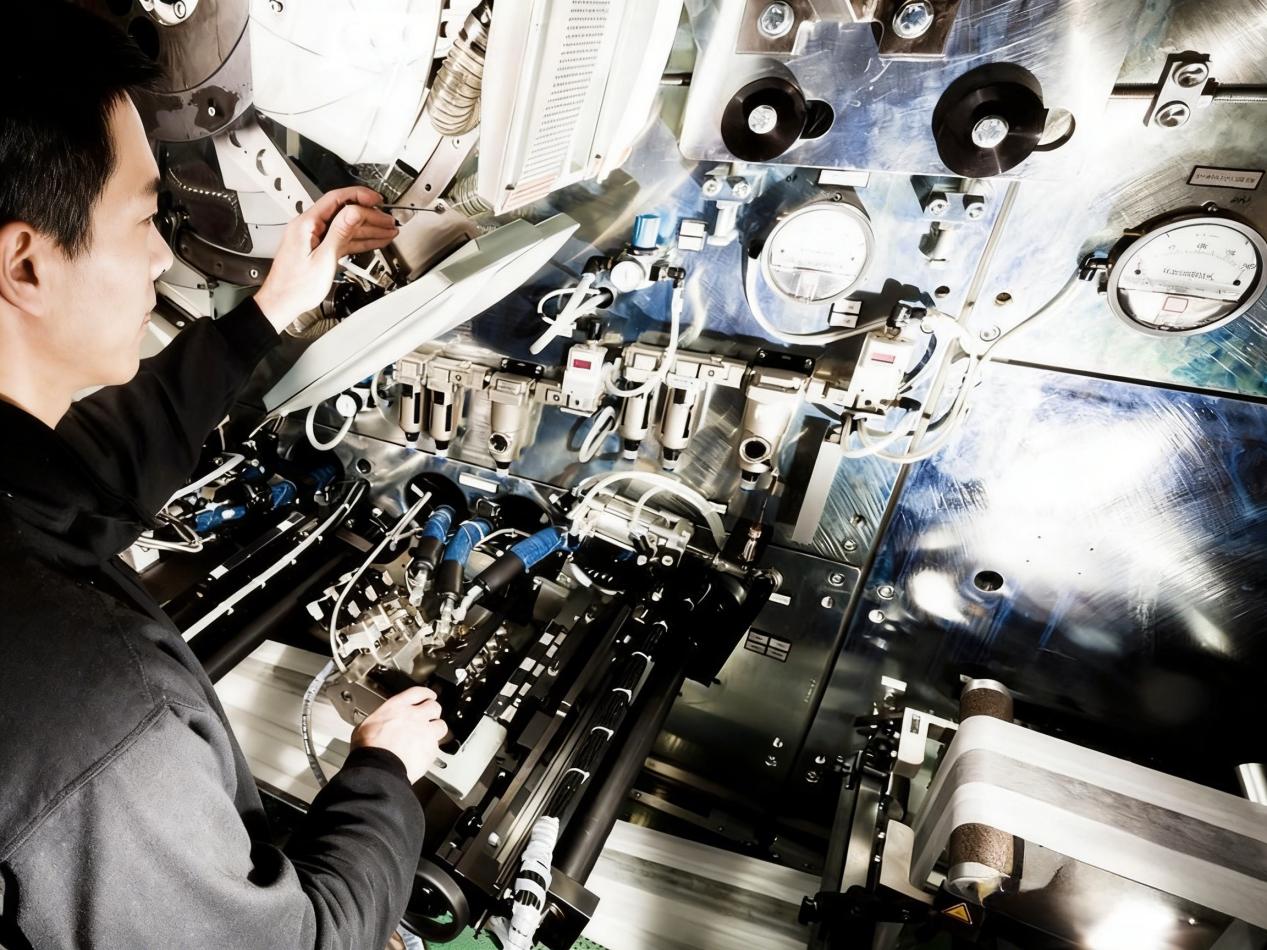
1. Regulatory Baseline: 2026 Global Standards for Medical & Hygiene Nonwovens
Key Regulatory Frameworks
Operating a refurbished nonwoven line requires meeting current compliance frameworks across target markets:
- ISO 13485:2016 Compliance: Governs medical device manufacturing quality systems, requiring verified process repeatability and strict contamination controls.
- FDA 21 CFR Part 820 & QMSR Alignment: Demands verifiable installation qualification (IQ) and operational qualification (OQ) records for all machinery producing Class I and II medical fabrics.
- EU MDR (2017/745): Imposes strict traceability on biocompatibility, requiring lines to run clean of unauthorized processing aids.
- EDANA and INDA Guidelines: Dictate absorption, fiber shed, and liquid strike-through benchmarks for baby diapers, adult incontinence, and feminine hygiene components.
Contamination Risk Thresholds
Medical and hygiene converters enforce near-zero tolerances for particulate and chemical contamination. Machine auditors must assess the equipment for three main hazards:
- Particulate Contamination: Carbon flakes from degraded polypropylene (PP) or polyethylene (PE) inside extruders or transfer manifolds.
- Volatile Organic Compounds (VOCs) and Odors: Residues from non-hygiene lubricants or reclaimed resin cross-contamination.
- Bioburden Ingress: Microorganisms harbored in dormant water circulation units, spunlace hydroentanglement circuits, or unsealed vacuum ducts.
2. Phase 1: Pre-Audit Documentation & Heritage Verification
Operational History & Maintenance Logs
A machine's past operational environment dictates its future failure points. Auditors must examine factory work shift logs and maintenance records across three key metrics:
- Historical Feedstock: Verify whether the previous operator ran 100% virgin medical-grade PP/PET or processed post-industrial regrind, calcium carbonate (CaCO3) fillers, or abrasive flame retardants that accelerate screw wear.
- Preventive Maintenance Logs: Check historical logs for critical assemblies, including vacuum blowers, gearboxes, melt pumps, and hydraulic roll-loading units.
- Operating Run Hours: Cross-reference recorded run hours on the HMI with motor duty logs and electrical power draw history to detect falsified operational metrics.
OEM Specifications vs. Current Modifications
Secondary market machinery frequently features unapproved modifications. The audit team must compare the physical asset against the original equipment manufacturer (OEM) general arrangement drawings.
- Identify third-party additions to extruder heating bands and heating circuits.
- Examine the die head and spinneret modifications to determine whether previous owners altered original capillary densities.
- Assess whether past electrical modifications comply with regional electrical codes (CE, UL, NFPA 79).
3. Phase 2: Mechanical & Thermal Precision Checklist
Polymer Extrusion & Spinning Systems (Spunbond/Meltblown)
The extrusion block and spinning beam form the functional core of spunbond, meltblown, and composite SMS lines. Mechanical wear here directly degrades web uniformity.
- Extruder Screw and Barrel: Use a bore micrometer to measure inner barrel wear and flight clearance. Excessive clearance causes polymer backflow, unstable melt pressure, and carbonization.
- Melt Pumps (Gear Pumps): Check gear tooth clearances. Worn gears cause pressure fluctuations that yield basis-weight variations across the running web.
- Die Heads and Spinnerets: Inspect meltblown die tips and spunbond spinneret capillaries under optical magnification. Look for orifice deformities, edge nicking, and incomplete ultrasonic cleaning.
- Air Knives and Attenuation Ducts: Check attenuation air slot dimensions. Warped air knives cause uneven filament draw and create heavy basis-weight bands.
Web Forming, Calendering & Bonding Units
Thermal bonding locks mechanical integrity into the web. In continuous high-speed converting, minute thermal or mechanical variations can ruin ultra-light hygiene materials.
- Calender Roll Geometry: Inspect the smooth and engraved roll surfaces using surface profilometry. Ensure run-out stays below 3 to 5 microns across the entire roll length.
- Thermal Oil Circulation: Use an infrared thermal imaging camera on heated rolls under operating temperatures. The temperature profile across the roll face must not drift beyond ±1.0°C.
- Spunlace Water Circuits: When auditing spunlace lines, inspect the high-pressure injector manifolds, strip slots, and closed-loop filtration circuits for corrosion, scale, and anaerobic biofilm build-up.
Tension Control, Slitting & Winding Systems
Lightweight medical and hygiene webs (spanning 10 to 25 gsm) shear and neck down under unstable web tension.
- Load Cells and Dancer Arms: Test the responsiveness of the tension feedback loop. The load cells must register micro-fluctuations instantly without mechanical sticking.
- Slitting Units: Examine shear-cut or razor slitting assemblies. Inspect for blade run-out and edge wobble, which cause micro-fraying and particulate shedding along web slit lines.
- Turret Winders: Verify splice efficiency and core transfers at maximum line speed to confirm roll edge alignment stays within ±1 mm.
Engineering teams partnering with KIMEPR get direct access to certified mechanical clearance logs, infrared calender mapping, and die-tip micro-inspections before buying.
4. Phase 3: Hygiene, Cleanroom & Cross-Contamination Inspection
Material Contact Surface Compatibility
All contact surfaces on hygiene-grade nonwoven equipment must resist corrosion and chemical reactions.
- Stainless Steel Verification: Confirm web guide rollers, suction boxes, and forming wires use AISI 304 or AISI 316L stainless steel. Carbon steel rollers with flaking nickel plating must be replaced immediately.
- Paint and Coating Integrity: Ensure framework located directly above open web pathways lacks flaking paint. Machine frames positioned over web pathways should feature hard anodized, nickel-plated, or stainless surfaces.
- Seals and Gaskets: Confirm all polymer and air seals use non-shedding, FDA-compliant elastomers (PTFE, EPDM, or fluoroelastomers) that do not break down into the web.
Lubrication & Pneumatic Systems
Uncontrolled hydraulic oil and pneumatic exhaust will contaminate medical-grade web batches instantly.
- NSF H1 Lubricant Conversion: Confirm all bearings, open gears, and drive units located near the web run on certified NSF H1 food- and medical-grade lubricants.
- Pneumatic Exhaust Filtration: Trace pneumatic valve terminals. Air exhaust must vent into dedicated filtration manifolds instead of exhausting directly over the web path.
- Hydraulic Seal Reliability: Test roll-loading hydraulic cylinders under maximum pressure for two hours. Any micro-weepage across piston seals warrants complete cylinder replacement.
Static Electricity & Dust Collection
Polypropylene fibers generate significant static charges, attracting airborne contaminants during winding.
- Verify the presence and output of high-frequency AC ionizing bars across web-forming, slitting, and winder intake zones.
- Audit trim-suction ducting for dead air zones where accumulated synthetic fluff can drop back into running rolls.
5. Phase 4: Electrical, PLC & Automation Modernization (The 2026 Lens)
PLC & HMI Legacy vs. Upgradeability
Sourcing obsolete industrial computers exposes operations to extended downtime risks.
- Platform Support: Identify the installed control base (e.g., Siemens S7-300/400, Rockwell SLC 500, Mitsubishi A-Series). Verify component availability and determine if replacement parts require an immediate migration to modern platforms like S7-1500 or ControlLogix.
- Drive System Integration: Inspect variable frequency drives (VFDs) and servo packs. Digital bus architectures (Profinet, EtherCAT) must maintain multi-axis synchronization without drift.
Inline Quality Inspection Systems
Modern hygiene and medical nonwoven production demands 100% automated inspection.
- Optical Vision Scanners: Check whether current inspection camera hardware can detect pinholes, insects, dark spots, and oil drops down to 0.5 mm at production speeds up to 600 m/min.
- Basis Weight Gauges: Inspect the radiometric (beta gauge) or non-radioactive (X-ray/infrared) scanner frame for mechanical track wear, sensor degradation, and synchronization lag across the web width.
2026 Cybersecurity & Data Integrity Requirements
Medical supply contracts require complete digital batch trace records.
- Verify that HMI software complies with FDA 21 CFR Part 11 requirements for encrypted electronic signatures, operator action tracking, and protected recipe storage.
- Ensure the system can export historical production data directly to factory
Manufacturing Execution Systems (MES) via OPC-UA protocols.
6. Phase 5: Commissioning, Trial Run & Validation (IQ/OQ/PQ)
Dry Run vs. Wet Run Testing
Never conclude an audit on static inspection alone. Run the machinery under full mechanical and process loads before finalizing release approvals.
- Dry Run Testing: Run all machine drives across the full speed range for four continuous hours. Measure bearing vibration signatures with Fast Fourier Transform (FFT) analysis to detect early raceway or gear pitting.
- Wet Run Extrusion Run: Feed virgin production polymer through the system. Measure motor torque stability, melt pump pressure stability, and die pressure variations over a continuous three-hour shift.
Acceptance Criteria for Medical Nonwovens
Extract samples directly from winder rolls during the loaded trial run and measure them against standard lab benchmarks:
- Basis Weight Uniformity (CV%): The cross-direction (CD) and machine-direction (MD) coefficient of variation must hold below 1.5% to 2.0% on light hygiene fabrics.
- Hydrostatic Head (AATCC 127): Essential for SMS medical barrier fabrics. Confirm the test web holds required water column pressures without premature barrier strike-through.
- Air Permeability and Tensile Profiles: Verify Frazier air permeability consistency across all roll slit widths. Check the MD/CD tensile ratio to ensure proper web laydown balance.
Used Nonwoven Machinery Audit Summary Matrix
- Extrusion & Die Section: Barrel clearances verified, zero polymer carbon buildup, spinnerets clear, melt pump variation < 1%.
- Bonding Section: Calender surface run-out < 5 µm, temperature uniformity within ±1.0°C, zero hydroentanglement biofilm.
- Hygiene Protection: Full 304/316L contact areas, NSF H1 food-grade lubricants installed, air exhaust directed away from web path.
- Control System: PLC architecture supported through 2030, inline optical vision functional, 21 CFR Part 11 recipe audit trails ready.
- Process Performance: Run tests achieve basis weight CV < 2.0%, stable hydrostatic head values, and verified vibration spectrums.
Frequently Asked Questions (FAQ)
Q1: What are the main points of failure when repurposing used nonwoven machinery for medical-grade products?
A1: The main failures stem from thermal profile variations along calender rolls, carbonized polymer contamination in die manifolds, and unrecorded mechanical run-out across high-speed rollers. Non-hygiene hydraulic leaks and outdated PLCs that lack recipe traceability also trigger audit rejections under ISO 13485 standards.
Q2: How much can converters save by buying refurbished nonwoven machinery instead of new lines?
A2: Converters save between 40% and 60% on initial equipment capital expenses. Refurbishing an existing European or high-end Asian spunbond/meltblown line also cuts delivery and installation lead times from 18 months down to 4 to 6 months.
Q3: How do we test for biofilm contamination in used spunlace equipment?
A3: Extract physical swab samples from injector manifold interiors, recovery piping walls, and final-stage cartridge housings. Subject the samples to adenosine triphosphate (ATP) bioluminescence and micro-culturing to verify zero bacterial or fungal colonies before beginning validation runs.
Q4: Can an older PLC system meet 2026 data integrity standards for medical nonwoven manufacturing?
A4: Legacy PLCs typically fail modern audit trail standards because they lack role-based access security, secure process logging, and encrypted interfaces. Converters usually retrofit older electrical cabinets with modern PLC architectures (such as Siemens S7-1500 or Allen-Bradley GuardLogix) to satisfy FDA 21 CFR Part 11 requirements.
Q5: What variance is acceptable for calender roll surface temperature on medical-grade lines?
A5: The temperature profile must not vary more than ±1.0°C across the entire working width. Greater variations create uneven thermal bonding, yielding soft spots, inconsistent tensile strength, and unpredictable barrier performance in finished medical fabrics.
Secure Your Machinery Investment with KIMEPR
Buying second-hand machinery shouldn't put your compliance at risk. With complete pre-purchase audits, mechanical testing, and retrofitting oversight, engineering teams can safely integrate refurbished systems into medical and hygiene production lines.
Download the Print-Ready Audit Sheet: Access our comprehensive 2026 Print-ready Used Nonwoven Machinery Audit Sheet (PDF/Excel) to guide your team through on-site plant inspections.
Need dedicated technical support for an upcoming machine acquisition? Contact KIMEPR today to consult our machinery audit specialists, request certified on-site engineering evaluations, or view our verified inventory of high-performance used nonwoven machinery.